 135-6073-0094
PRODUCT CENTER
Cutting Tool Screws
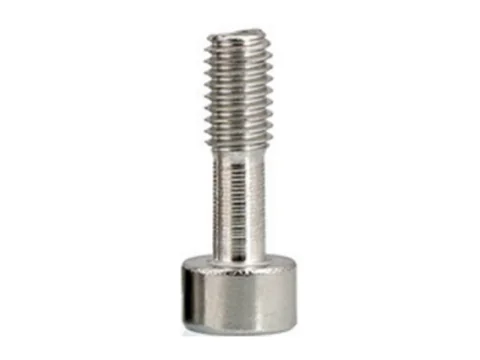
TORX PLUS 8IP tool screw in M2.5×6.5 with 0.45 mm pitch, for
TORX PLUS 8IP Tool Screw|M2.5×6.5 (0.45 Pitch)
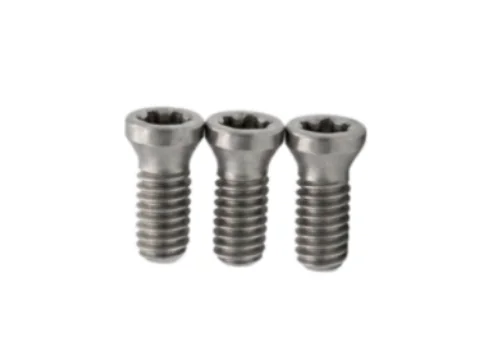
- Installationtorqued to the tool maker's value
- StandardGB/T 3098.1, ISO 16047
- Typical substrateindexable carbide inserts
- Key inspectionshead cone, recess, thread gauging, hardness
- Thread SizeM2.5 × 6.5mm
- Drive TypeTorx Plus 8IP
Product overviewOverview
A tool screw holds the carbide insert in its pocket by preload: the resulting friction resists the cutting force. At M2.5 the screw develops little clamp force, so seat contact and engaged thread length matter more than torque. A worn 8IP bit rounds the socket before the screw reaches its rated torque, and a rounded socket is the usual reason an insert starts to move.
installed by torqued to the tool maker's value.
Key featuresFeatures
- Small socket wears first: replace 8IP bits on a counted schedule.
- Head-to-thread coaxiality is controlled to avoid tilting the insert during clamping.
- Head diameter, length, recess depth and thread length can be made to the holder drawing.
- Alloy steel quenched and tempered to class 12.9, with strength and hardness to GB/T 3098.1.
Typical applicationsApplications
- Drill and reamer clamping
- Swiss-type lathe tool stations
- Fine boring and adjustment heads
Selection notesSelection
Judge the assembly by insert movement under cut, not by torque alone; torque scatter at this size is larger than the difference between a good and a loose seat.
Frequently asked questionsFAQ
Why do 8IP sockets round off?
What matters during installation of the TORX PLUS 8IP Tool Screw|M2.5×6.5 (0.45 Pitch)?
| Thread Size | M2.5 × 6.5mm |
|---|---|
| Drive Type | Torx Plus 8IP |
| Standard | GB/T 3098.1, ISO 16047 |
| Drive | star recess |
| Installation | torqued to the tool maker's value |
| Typical substrate | indexable carbide inserts |
| Key inspections | head cone, recess, thread gauging, hardness |
Torque-to-clamp-force is measured to ISO 16047 to confirm lot-to-lot friction stability.Material certificates and dimensional records accompany each lot; material and dimensional records are supplied per batch.