 135-6073-0094
PRODUCT CENTER
Cutting Tool Screws
Cutting tool screw in alloy tool steel at property class 12.
TORX PLUS Cutting Tool Screw
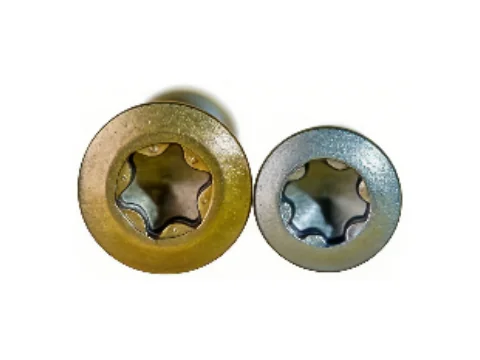
- MaterialAlloy Tool Steel
- Installationtorqued to the tool maker's value
- StandardGB/T 3098.1, ISO 16047
- Typical substrateindexable carbide inserts
- Key inspectionshead cone, recess, thread gauging, hardness
Product overviewOverview
The head cone or face centres the insert in its pocket, and the star recess delivers torque through a small head diameter. The coating follows cutting temperature: TiN is used up to roughly 600 °C in general turning, TiAlN resists oxidation to about 800 °C where the insert runs hot. Coating also lowers thread friction, so the same torque produces a higher clamp force than an uncoated screw.
Material: Alloy Tool Steel. It is tightened to the torque the tool maker publishes.
Key featuresFeatures
- TiN for general turning, TiAlN where the insert runs hot.
- Alloy steel quenched and tempered to class 12.9, with strength and hardness to GB/T 3098.1.
- Star recess transmits the tool maker's torque without cam-out in a restricted head diameter.
- Head cone seats the insert concentrically, so tip position repeats after a change.
Typical applicationsApplications
- Swiss-type lathe tool stations
- Fine boring and adjustment heads
- CNC turning insert clamping
Selection notesSelection
Use the coated-screw torque value from the tool maker: the same setting on a coated and an uncoated screw gives different clamp force.
Frequently asked questionsFAQ
Does the coating change the torque setting?
What matters during installation of the TORX PLUS Cutting Tool Screw?
| Material | Alloy Tool Steel |
|---|---|
| Property Class | Grade 12.9 |
| Surface Treatment | TiN / TiAlN coating |
| Standard | GB/T 3098.1, ISO 16047 |
| Drive | star recess |
| Installation | torqued to the tool maker's value |
| Typical substrate | indexable carbide inserts |
| Key inspections | head cone, recess, thread gauging, hardness |
Head cone angle and recess are checked on a profile projector, threads gauged 6g on every part.We recommend a pilot assembly at the actual torque and mating part before locking the process parameters for volume.