 135-6073-0094
PRODUCT CENTER
Locking Products
Ultra-thin self-clinching nut: a low-height part for thin sh
Ultra-Thin Self-Clinching Nut
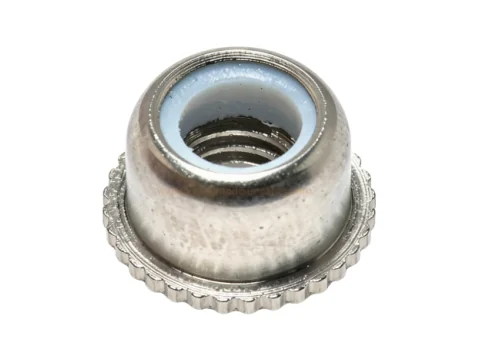
- MaterialSpring Steel 65Mn / Stainless Steel 304
- Installationpressed into a prepared hole with a clinching press (single side)
- StandardGB/T 90.1 (acceptance), customer drawing
- Typical substratecold-rolled steel, stainless and aluminium sheet 0.5–3 mm
- Key inspectionspush-out, torque-out, face flushness
Product overviewOverview
A self-clinching nut is held by cold flow, not by thread friction. A clinch nut is held by sheet material displaced into an undercut, so a thinner nut leaves less room for that material and push-out falls quickly as the gauge drops. On sheet around 1 mm both hole size and press force have to be held tightly, because there is little margin to correct either.
Material: Spring Steel 65Mn / Stainless Steel 304. It is pressed into a prepared hole with a clinching press, working from one side.
Key featuresFeatures
- Because the nut is thin, the undercut has little wall to work with and both hole size and press force must be held to the drawing.
- Annular undercut and knurl: sheet metal flows in to form a mechanical interlock.
- Push-out and torque resistance come from metal shear and knurl bite.
- Pressed in, the head finishes flush and the panel can be closed against a flat gasket or a sliding cover.
Typical applicationsApplications
- Server and telecom rack panels
- Sheet-metal chassis thread bosses
- Battery pack enclosures
Selection notesSelection
Verify push-out on the production gauge rather than on a thicker trial piece; performance does not scale down with nut height.
Frequently asked questionsFAQ
Can a standard clinch nut be used on thin sheet?
What matters during installation of the Ultra-Thin Self-Clinching Nut?
| Material | Spring Steel 65Mn / Stainless Steel 304 |
|---|---|
| Surface Treatment | Zinc-plated / Black oxide |
| Standard | GB/T 90.1 (acceptance), customer drawing |
| Installation | pressed into a prepared hole with a clinching press (single side) |
| Typical substrate | cold-rolled steel, stainless and aluminium sheet 0.5–3 mm |
| Key inspections | push-out, torque-out, face flushness |
Push-out and torque tests are sampled per lot, with failure load recorded.We recommend a pilot assembly at the actual torque and mating part before locking the process parameters for volume.