 135-6073-0094
Thread Inserts
Thread Inserts
self-tapping insert in single-slot, three-slot and
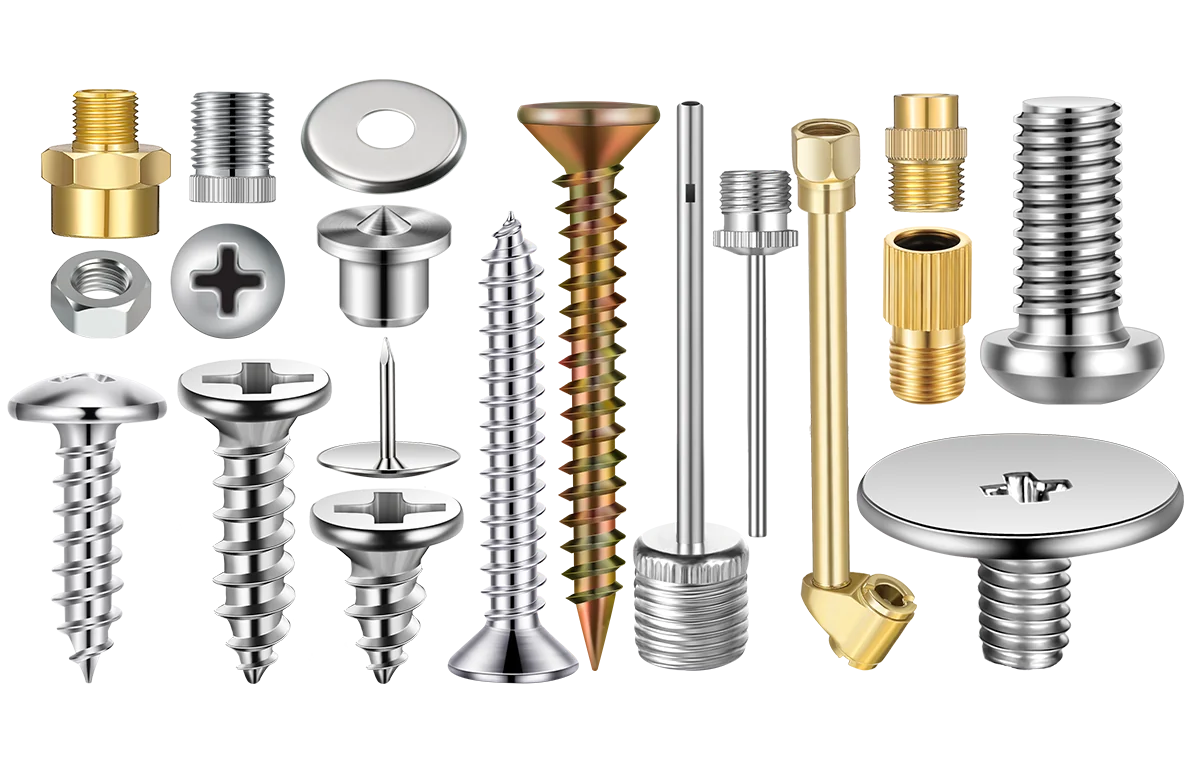
Self-Tapping Inserts | M2-M4 Slotted, Three-Slot & Hex Drive
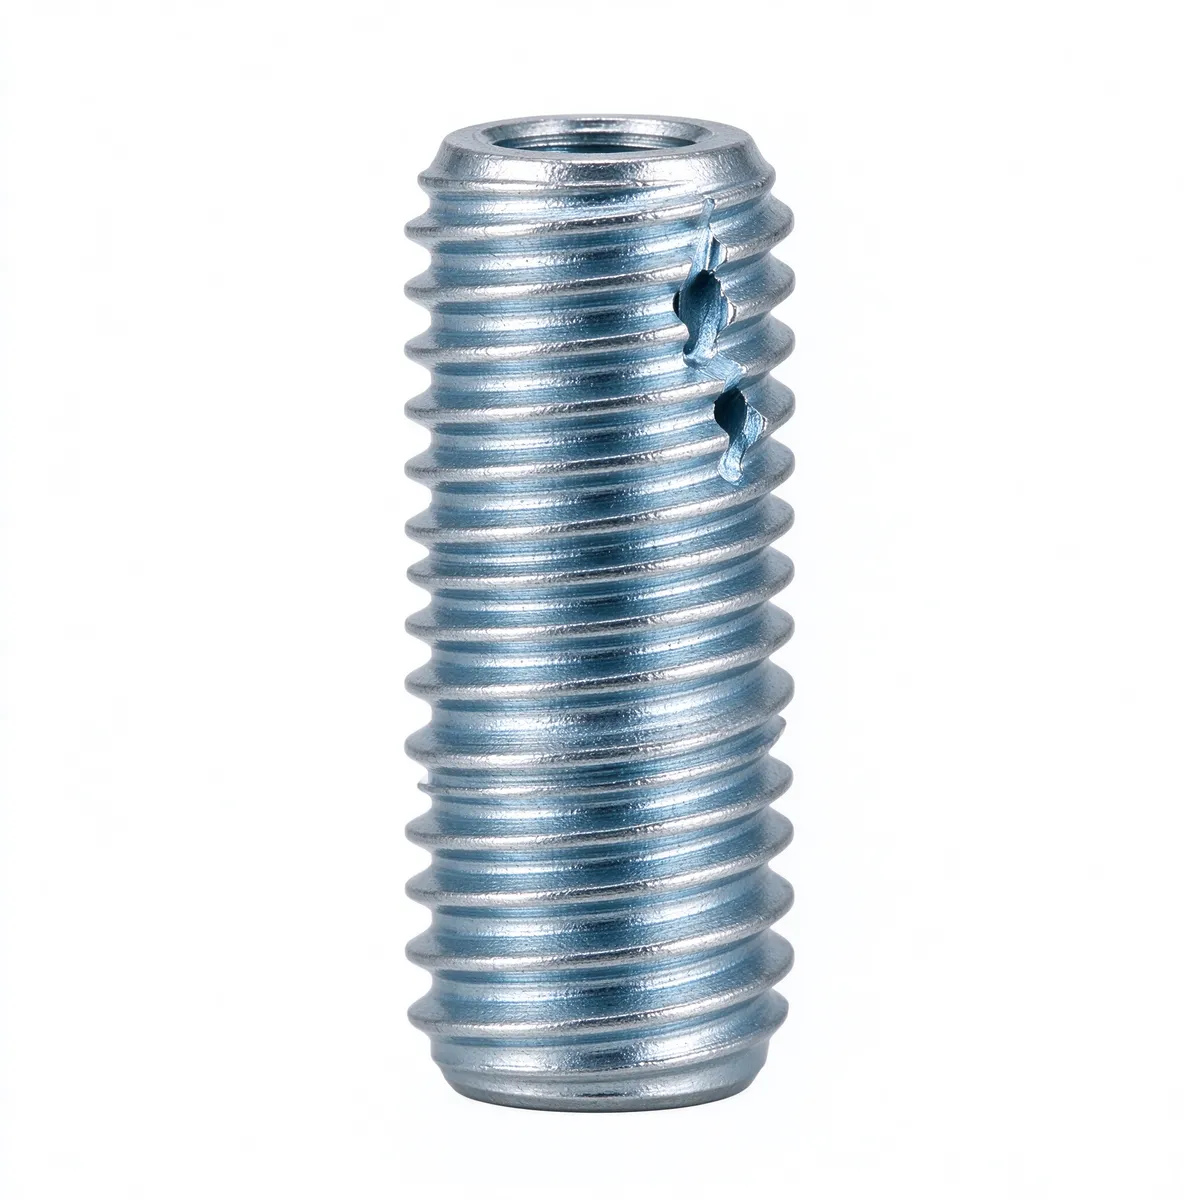
- Size rangeM2-M4
- MaterialCarburized steel
- FinishBlue zinc passivation
- InstallationSetting tool or hex key
- StandardGB/T 197 (6H internal thread), company standard
- Typical substratealuminium, zinc alloy, engineering plastics
Product overviewOverview
The external thread of a self-tapping insert is a cutting tool. The slot pattern decides how the insert cuts and how it is driven: a single slot cuts with one cutting edge and needs a setting tool, three slots distribute the cut and reduce driving torque, and the hex-drive versions can be set with a key where a tool cannot reach. Choice follows the base material and the access, not the thread size.
This page covers M2-M4 in Carburized steel, with blue zinc passivation as the standard finish. It is installed by Setting tool or hex key.
Key featuresFeatures
- Slot pattern chosen by base material and access, not by thread size.
- Cuts its own thread in a drilled hole, eliminating the tapping operation.
- Slotted type clears chips, making it suitable for blind and deep holes.
- Three-hole type cuts at the face for smoother torque on automated equipment.
Typical applicationsApplications
- Aluminium housings
- Zinc die-cast thread repair
- Engineering plastic reinforcement
Selection notesSelection
Match the type to the base material: three-slot for tough alloys where driving torque is high, hex drive where access is limited, single slot for general use with a setting tool.
Frequently asked questionsFAQ
Which slot type should I choose?
What matters during installation of the Self-Tapping Inserts | M2-M4 Slotted, Three-Slot & Hex Drive?
| Size range | M2-M4 |
|---|---|
| Types | S single slot / SB three slot / SI single slot hex / SBI three slot hex |
| Material | Carburized steel |
| Finish | Blue zinc passivation |
| Thread standard | ISO metric |
| Installation | Setting tool or hex key |
| Standard | GB/T 197 (6H internal thread), company standard |
| Head style | hex head |
| Drive | slotted |
| Typical substrate | aluminium, zinc alloy, engineering plastics |
Internal threads are gauged 6H on every part; external thread form and slot position are sampled.We recommend a pilot assembly at the actual torque and mating part before locking the process parameters for volume.